Well after cleaning the bearings The scoring in them was a little more than I felt comfortable with, I could feel them with my finger nail. Sorry I forgot to take pics of them, once I started working on them I just got consumed and hyper focused. So I mounted them in the head stock and just put the bolts in finger tight to hold the bearings shape round and square to the head stock. Then I ran a cylinder hone through them by hand just untill most of the ridges where gone. I then polished them with some 600 grit paper just untill the scratches where gone. Once this was all done I buffed the bearing surfaces on the spindle and assembled everything in the head stock with new capillary oil wicks. Then I installed .0225" of the shims I made at the four contact points of the bearing caps. I installed the caps and the dovetail adjuster screws. Tightened everything down and tested the bearing clearance, very important for proper oiling of the bearings and spindle.
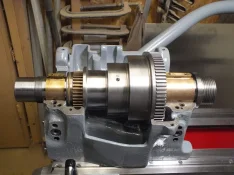
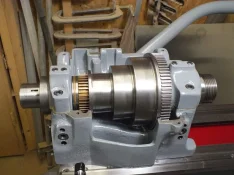
This is what the spindle was supposed to look like when I first took it apart, see the little bronze dove tail adjusters on top of the bearings, they are very important!
[attachment=13310]
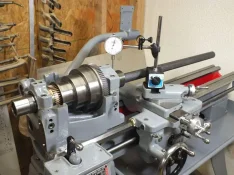
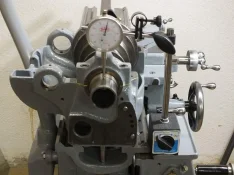
This is the set up for testing for bearing clearance, mag base with a .001 dial indicator and a 1 1/4" solid bar to lift up with.
[attachment=13311]
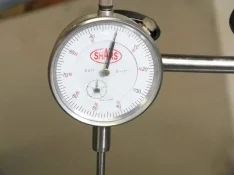
Indicator set to zero.
[attachment=13312]
And the set up for the other end, being sure to have the indicator tip on a smooth surface of the spindle and not the threads.
[attachment=13313]
Hear you can see the take up nut and hardened washer installed, It is set to .001" of play
[attachment=13314]
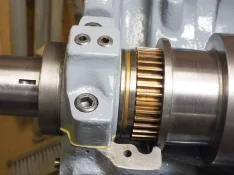
Here you can see the take up bearing next to the bronze gear and the shims sticking out from under the bearing caps, I would rather have them too big than too small. It was important to not have them stick out on the sides though so they would not rub on the take up bearing or lock nut ring.
[attachment=13315]
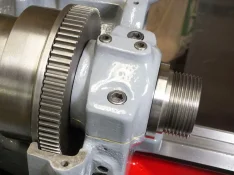
A pic of the bull gear and spindle nose.
[attachment=13316]
I ended up testing the clearance three times and finaly ended up with .0185" of shims for a perfect setting of .001" of clearance. the spindle turnes very easy by hand and has less than .0005" of run out.

This was the most important part of the rebuild and I paid the most attention to it. I am glad it is done and can now get on with the rest of the restore.